An ageing primary mineral sizer seldom fails in a single, obvious moment. More often, it drains capital through blockages, rushed tooth changes, a slowed feeder, and oversize material. Each incident can look manageable; across a year, the cost appears in lost availability, overtime, spare parts, unstable production, and missed tonnes.
For a mine or coal-handling plant, replacement should not rest on machine age alone. The test is whether the sizer still provides safe, predictable throughput and controlled top size under today’s duty. In coal, lignite, limestone, gypsum, phosphate, oil shale, and similar materials, this stage governs the flow of the whole circuit.
Here are five signs that upgrading has become a cost-reduction and operational-modernisation project rather than a discretionary capital purchase.
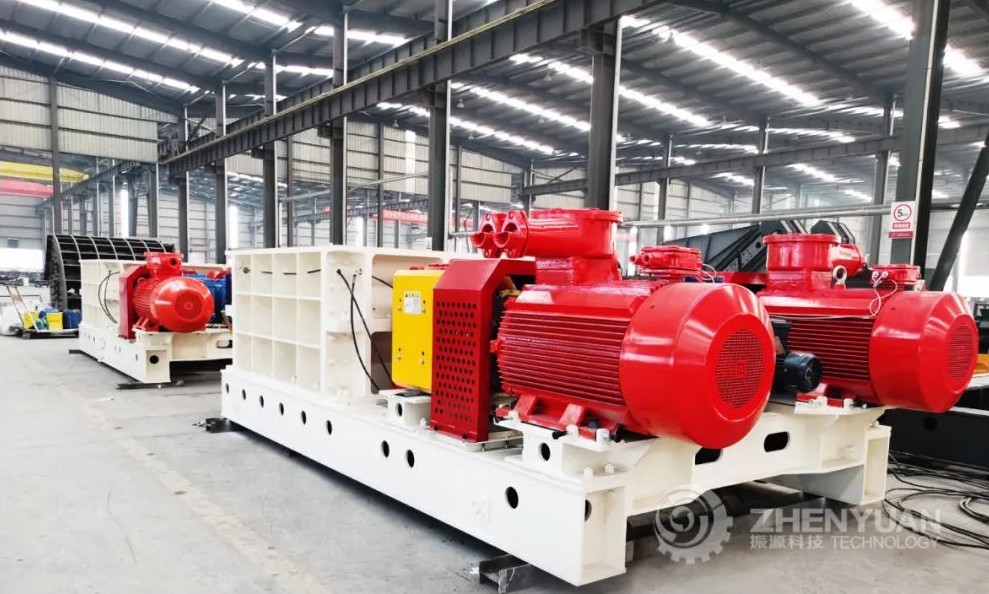
1. The Primary Mineral Sizer Cannot Sustain the Required Throughput
Nameplate capacity is only a starting point. If operators regularly reduce feeder speed, bypass large lumps, or pause the upstream conveyor to keep the sizer running, actual capacity is already below the requirement. A machine that runs but prevents the apron feeder from delivering its planned rate is constraining the entire plant.
Compare planned tonnes, actual tonnes, running hours, and time lost to flow restrictions—not just the monthly production total. Specify any replacement from current feed distribution, density, abrasiveness, moisture, peak capacity, required top size, and tramp-material risk.
2. Maintenance Has Become a Reaction Instead of a Plan
Wear parts are expected in primary crushing. Emergency repairs should not be. When teeth, liners, fasteners, seals, bearings, or drive components are changed mainly after a production stop, maintenance is being dictated by the machine rather than managed by the site.
Count every event: lost tonnes, labour, lifting, freight, safety exposure, and downstream disruption. Replacing only the worst visible tooth can seem economical, yet mismatched profiles create uneven loading and shorten the life of the set.
A modern primary mineral sizer can make service work more predictable through accessible wear components, reliable tooth retention, monitoring points, and a maintainable drive. Tooth material still needs a balance of wear resistance and impact toughness. The aim is planned maintenance based on actual feed and a measured trend.
3. Cost per Tonne Is Climbing While Output Stays Flat
Rising or erratic motor load at the same feed rate is an important warning, even though energy use must always be viewed alongside changing material conditions. Worn teeth can lose their grip. Packed fines, restricted discharge, off-centre feed, and repeated re-crushing can increase torque without adding saleable output. The plant then pays more power and labour per tonne for less stable crushing.
Track kWh per tonne with motor current, throughput, stoppages, and feed characteristics. A wetter coal seam or harder mining horizon may alter demand, but a sustained adverse trend warrants investigation. Review the sizer, feeder, transfer chute, and discharge as one system. The credible energy benefit is fewer choke events, restart cycles, and unnecessary rehandling.
4. Product Size Drift Is Burdening Downstream Equipment
When a primary mineral sizer produces more oversize or excess fines, the financial effect moves down the line. Oversize can upset a screen, overload a conveyor, or force secondary equipment to work harder. Too many fines can increase dust, complicate material handling, and affect screening or beneficiation performance.
The change is usually gradual: tooth profiles wear, clearances drift, and breaker bars or liners lose their intended geometry. Simply closing a gap or increasing speed can increase wear and fines if it is not engineered for the material.
Use representative product sampling and screen analysis to establish the actual size distribution. Then inspect tooth height and consistency, roll-to-roll and roll-to-breaker clearances, and the feed pattern across the roll width. Select a new primary mineral sizer for the desired top size and downstream process requirements, not only for a quoted reduction ratio.
5. The Controls Do Not Support Modern Operating Discipline
Many legacy sizers rely on an operator recognising changed sound, vibration, or discharge before a trip occurs. Experience is valuable, but without drive load, bearing temperature, lubrication status, or fault history, it is an incomplete picture.
Modernisation can add drive-load monitoring, bearing-temperature alarms, lubrication status, controlled reversing, feeder-sizer interlocks, and maintenance trend data. Protection and reversing functions remain safeguards; they must follow the manufacturer’s procedure and never substitute for correcting unsuitable feed.
Make the Upgrade Case on Total Cost of Ownership
Build the decision around a duty audit, not a brochure comparison. Gather feed samples, moisture, lump size, actual and peak tonnes per hour, product-size data, power trends, downtime causes, wear consumption, and the limits of the feeder, chutes, structure, and downstream conveyors. This shows whether the bottleneck is the sizer or an interface.
Then price the status quo: lost tonnes, repair hours, spares, energy, labour, secondary-crushing load, and operational risk. The right project may include chute improvements, feeder control, or metal detection. A primary mineral sizer is a control point, not an isolated machine.
Capital discipline is not waiting for catastrophic failure. It is recognising when an obsolete bottleneck costs more to operate than a modern, correctly specified primary mineral sizer costs to own. The result should be steadier feed, planned maintenance, controlled product size, and more productive operating hours.
FAQ
Upgrade a Primary Mineral Sizer when repairs no longer restore dependable throughput, availability, or product size. Compare the cost of downtime, repairs, wear parts, power, and downstream disruption with a correctly engineered replacement.
Provide material type, abrasiveness, moisture, clay content, density, maximum lump size, feed distribution, average and peak capacity, required top size, and tramp-metal risk. Feeder, chute, conveyor, and downstream-process details are also important.
Often, yes. The Primary Mineral Sizer and complete feed system must be matched to representative material. Tooth geometry, roll spacing, feed rate, chute trajectory, and discharge capacity affect performance with wet coal, clay-bearing ore, or sticky limestone.
A Primary Mineral Sizer upgrade can improve wear-part access, stabilise material flow, provide condition data, and match tooth materials to the duty. Savings are strongest when it also corrects off-centre feed, excessive drop height, and tramp-material exposure.